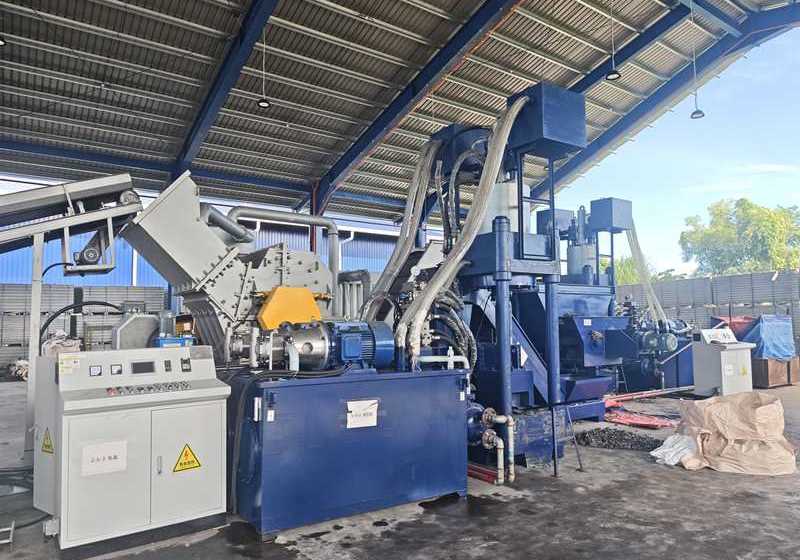
Vertical Pre-Press Briquette Press
Vertical Metal Chip Briquetter with Pre-Compression
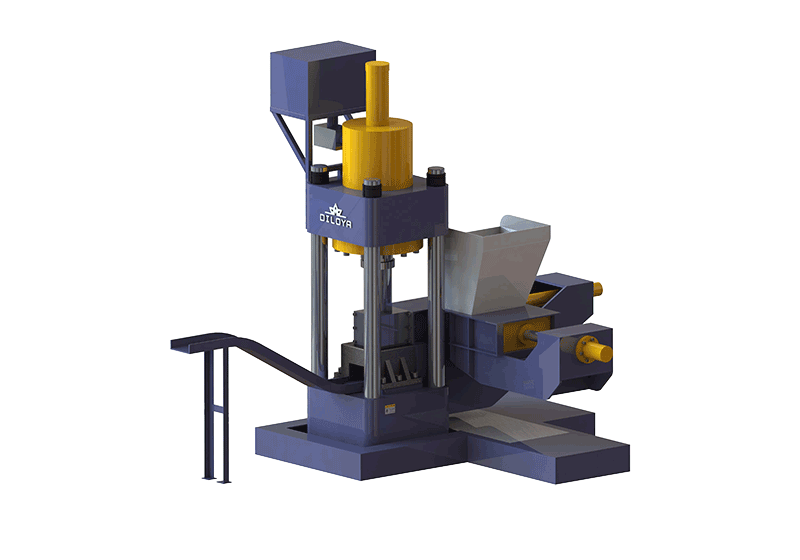
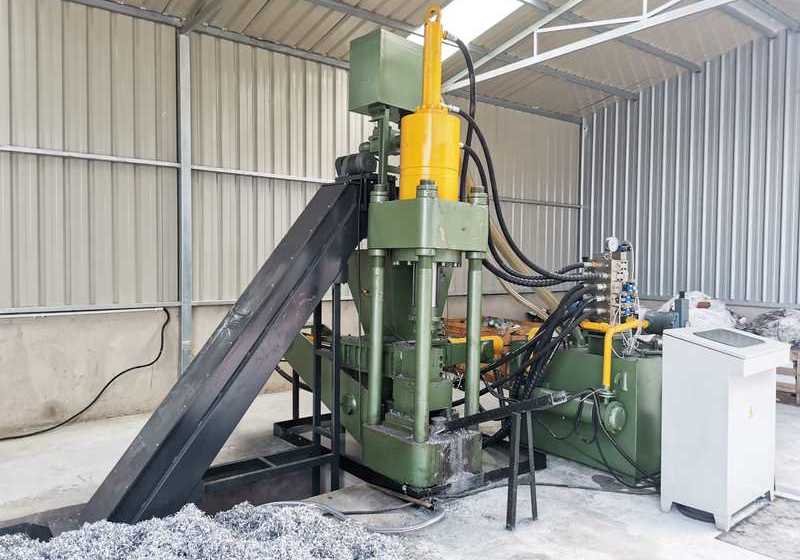
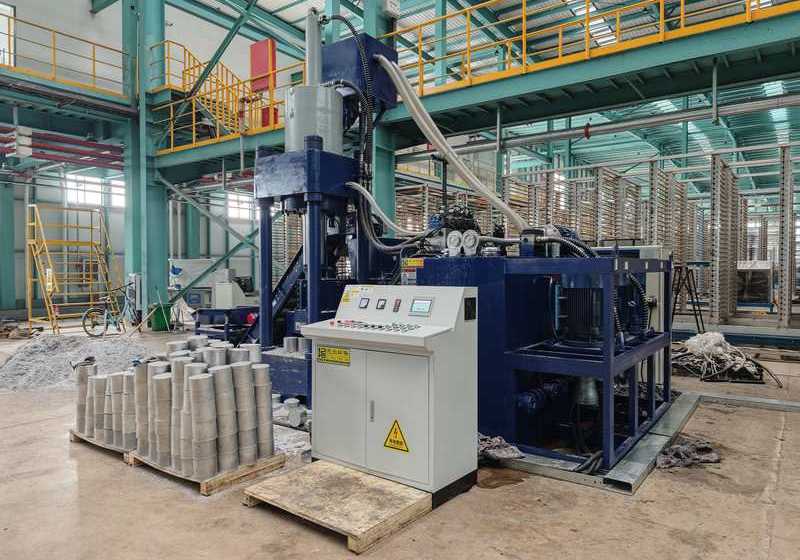
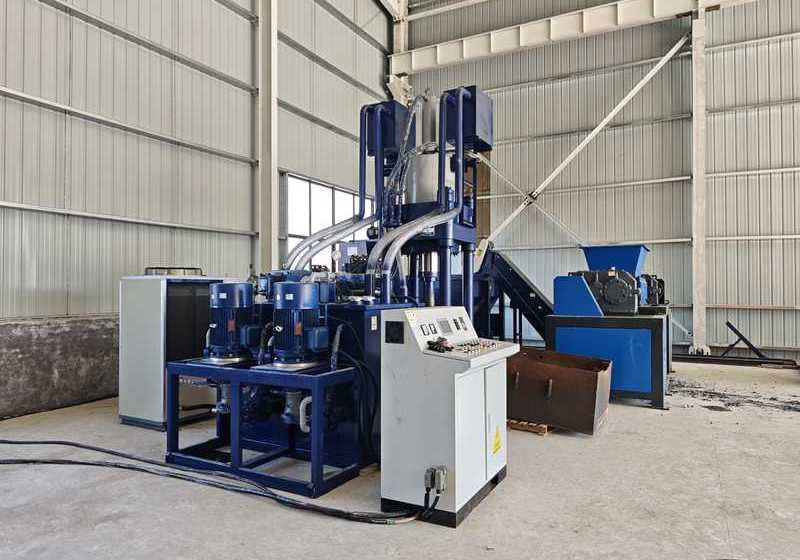
The DILOYA Vertical Pre-Press Briquette Press adds a pre-compression stage before final vertical hydraulic pressing. It is designed to control bulky or springy, prepared metal chips and form consistent briquettes for handling and recycling.
- Design
- Vertical Pre-Press
- Brand Name
- DILOYA
- Output Capacity
- 500-3000kg/Hour
- PLC Brand
- Mitsubishi
- Power supply
- Customized
- Support
- Engineering And After-sales
Description
The DILOYA Vertical Pre-Press Briquette Press combines preliminary compaction with final vertical hydraulic pressing. Loose metal chips can be bulky, irregular or springy, making them difficult to feed consistently into a forming chamber. The pre-press stage reduces the initial volume and creates a more controlled charge before the main vertical ram forms the briquette. This is the feature that distinguishes it from a standard vertical briquetting press.
1> Two-Stage Compaction
Prepared chips enter the feeder, where the pre-press mechanism compresses or meters them into the briquetting chamber. The main ram then applies final pressure to form the block. After discharge, the system resets for the next charge. The exact cylinder arrangement, feeding method and cycle sequence depend on the selected model and should be confirmed against drawings and chip tests.
2> Material Suitability
Separately sorted aluminium, copper, brass, cast-iron and other compatible machining chips may be considered. Pre-pressing can improve charge control, but it does not replace proper chip preparation: long tangled turnings may still need size reduction, and tramp material, mixed alloys or hazardous contamination must be removed. Moisture and cutting fluid content influence block stability and any fluid-recovery requirement.
3> Engineering the Right Line
DILOYA should assess representative chip samples, loose bulk density, hourly volume, desired briquette size, available headroom and handling equipment. Pre-press stroke, main force, chamber size, controls, conveyors and fluid collection are then configured for the project. Benefits should be evaluated against the actual feed material rather than assumed from the pre-press label alone.
Advantage
> Pre-compression stage: reduces loose chip volume before the final press stroke.
> Improved charge control: helps meter bulky or springy material into the forming chamber.
> Vertical final pressing: applies hydraulic force to form regular briquettes.
> Cold recycling process: consolidates chips without melting them.
> More orderly handling: briquettes simplify counting, weighing, storage and shipment.
> Material flexibility: suitable aluminium, copper, brass and ferrous chips can be assessed separately.
> Coordinated operation: pre-press, main ram and discharge can run in a defined control sequence.
> Configurable preparation: feed, chip breaking and fluid collection can be selected as the material requires.
Parameter
Please find below specification of different models:
| Model | BPP150 | BPP250 | BPP360 | BPP500 | BPP630 |
|---|---|---|---|---|---|
| Briquette Size | Φ100x(70-90)mm | Φ120x(80-100)mm | Φ140x(80-100)mm | Φ160x(90-110)mm | Φ180x(100-120)mm |
| Briquette Weight | Alu: 1.1-1.4kg Steel: 2.4-3.1kg Copper/Brass: 3.3-4.2kg | Alu: 1.8-2.2kg Steel: 4.1-5kg Copper/Brass: 5.4-6.8kg | Alu: 2.4-3.1kg Steel: 5.5-6.9kg Copper/Brass: 7.4-9.2kg | Alu: 3.6-4.4kg Steel: 8.1-9.9kg Copper/Brass: 10.8-13.2kg | Alu: 4.6-5.6kg Steel: 10.3-12.6kg Copper/Brass: 13.7-16.8kg |
| Output Capacity | Alu: 0.15-0.2t/h Steel: 0.4-0.5t/h Copper/Brass: 0.5-0.6t/h | Alu: 0.27-0.35t/h Steel:0.6-0.8t/h Copper/Brass: 0.8-1t/h | Alu: 0.4-0.5t/h Steel: 0.85-1t/h Copper/Brass: 1.1-1.4t/h | Alu: 0.55-0.7t/h Steel: 1.2-1.5t/h Copper/Brass: 1.6-2t/h | Alu: 0.7-0.9t/h Steel: 1.6-1.9t/h Copper/Brass: 2.1-2.6/h |
| Motor Power | 22kw | 18.5kw | 30kw | 2x22kw | 2x30kw |
| Cycle Time | 25s | 20s | 20s | 20s | 20s |
| Control | PLC Control | PLC Control | PLC Control | PLC Control | PLC Control |
| Cooling System | Oil Chiller | Oil Chiller | Oil Chiller | Oil Chiller | Oil Chiller |
| Main Cylinder | 1500kn | 2500kn | 3600kn | 5000kn | 6300kn |
| Speed Cylinder | 200kn | 300kn | 300kn | 500kn | |
| Pre-Press Cylinder | 80kn | 80kn | 150kn | 300kn | 300kn |
| Feed Cylinder | 80kn | 80kn | 100kn | 120kn | 150kn |
| Push Cylinder | 200kn | 200kn | 230kn | 300kn | 500kn |
We can customize the baler machine according to your special requirements.
Application
The DILOYA BPP Series vertical pre-press briquetting machine can press below mateirals:
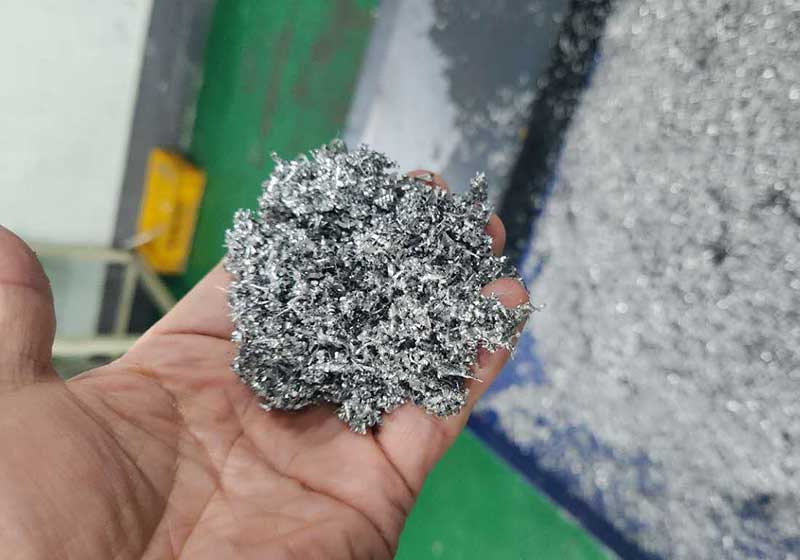
Aluminium Chips
Aluminium Chips are precision-processed from pure aluminum and aluminum alloy via CNC turning and milling. Strictly sorted, cleaned and dried, these chips feature uniform shape, low oxidation and zero sundry impurities. As premium recycled aluminum raw materials, they deliver stable metallurgical and physical properties, ideal for aluminum smelting, alloy production, chemical processing and thermal conduction applications with high cost performance.
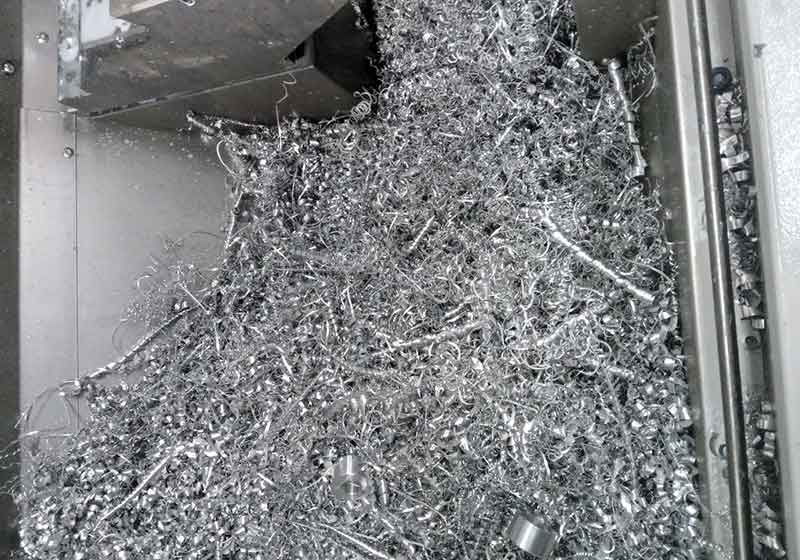
Aluminium Turnings
Aluminium Turnings are lightweight, spiral-shaped metal chips generated during machining, drilling and milling. DILOYA briquetting and baling systems compact loose turnings into dense, manageable blocks, helping reduce storage volume, improve transport efficiency and support aluminium recovery.
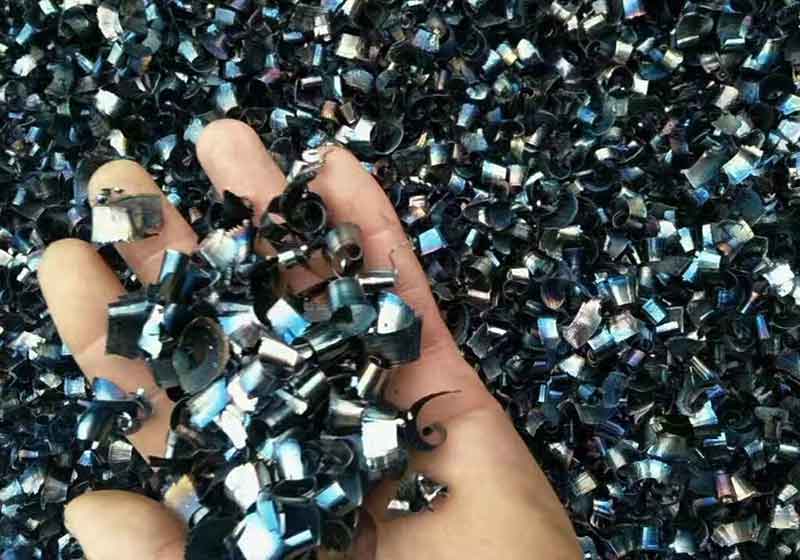
Steel Chips
Steel chips from turning, milling, drilling and sawing are loose, oily and difficult to handle efficiently. DILOYA hydraulic briquetting presses compress carbon-steel, cast-iron and alloy-steel swarf into dense cylindrical briquettes, recovering part of the retained cutting fluid while improving storage, transport and furnace feeding. This application is intended for briquetting only.
Steel Shavings
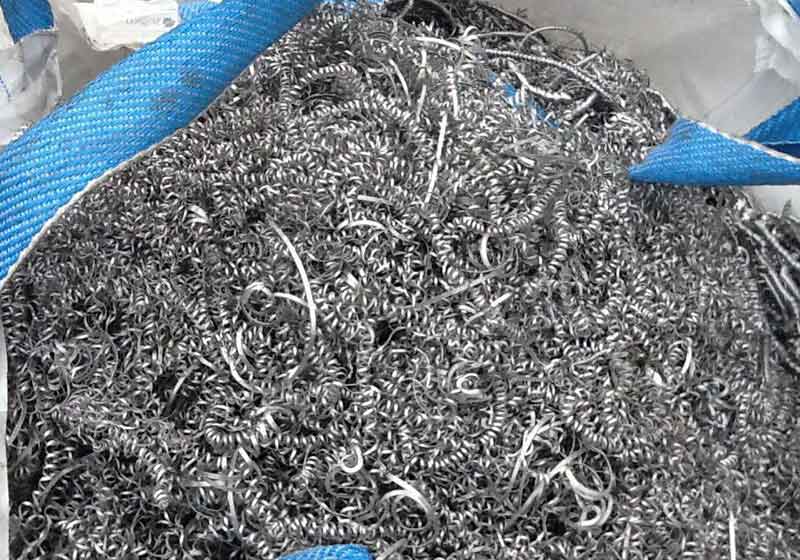
Steel shavings are long, curled machining residues that interlock into bulky nests and retain cutting fluid. DILOYA can compress foldable shavings directly into rectangular transport bales, or shred long tangled nests into short uniform feed before hydraulic briquetting. Process selection depends on shaving geometry, fluid content, required density and downstream furnace specifications.
Copper Chips
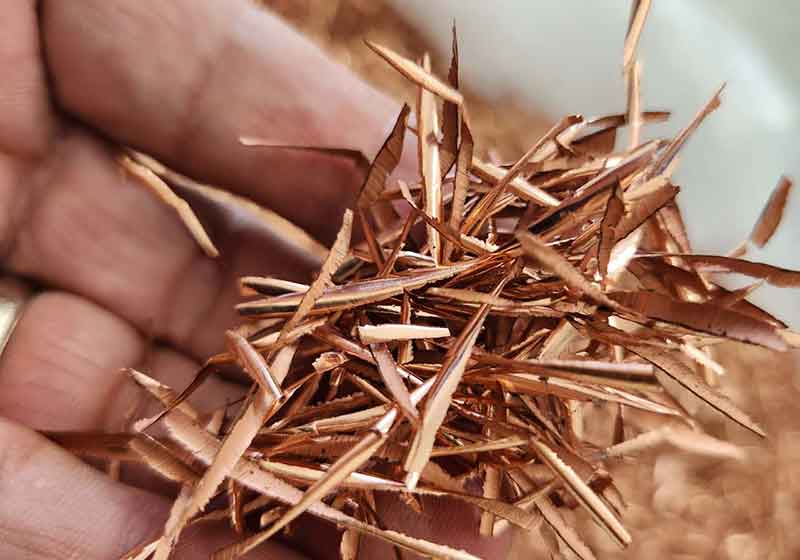
Copper chips from turning, milling and drilling are valuable but bulky, oily and easy to lose during handling. DILOYA hydraulic briquetting presses compact separated copper machining chips into dense binder-free cylinders while recovering part of the retained fluid for efficient storage, shipment and remelting. This Copper&Brass Scrap application is intended for briquetting only.
Brass Chips
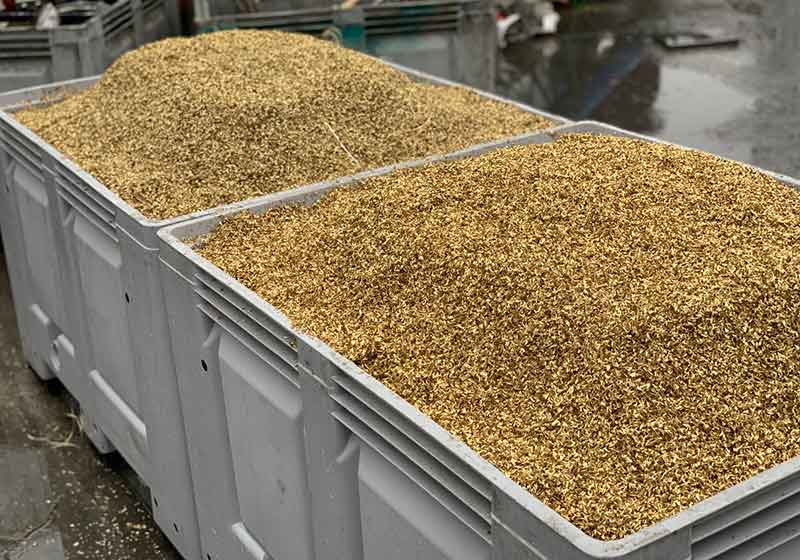
Brass chips from machining valves, fittings and alloy components are loose, oily and difficult to transport efficiently. DILOYA hydraulic briquetting presses compress sorted brass swarf into dense binder-free cylinders, recovering part of the retained cutting fluid while improving grade control, storage, shipment and furnace charging. This Copper&Brass Scrap application is intended for briquetting only.
FAQ
What is the purpose of pre-compression on a briquetting press?+
Pre-compression addresses the filling problem created by bulky low-density chips before the main pressing stage. Its value is determined by accepted briquette mass and sustained output, not the size of the loose charge alone. Vertical Pre-Press Briquette Press is a relevant arrangement to evaluate with the actual feed and complete cycle.
The useful result should be measured as accepted briquette mass and sustained production. A larger loose charge is not a benefit if the rest of the feeding cycle cannot supply it reliably.
Its effect depends on feed geometry, chamber design and the selected cycle. It is not a guaranteed output increase for every material. Evaluate briquette mass and sustained production with the actual chips rather than assuming identical gains across all alloys.
Which press arrangement suits fluffy aluminium or brass chips?+
For fluffy aluminium or brass chips, receiving volume and reliable charging can limit performance before maximum force does. Assess an appropriate pre-compression arrangement, such as Vertical Pre-Press Briquette Press, using measured loose bulk density and chip shape. The result must be established for each alloy rather than inferred from a visually similar swarf pile.
Provide chip shape, bulk density and expected output. Prepared steel swarf and Copper Chips may need different settings even when they look similarly fluffy. Material trials help establish the required charge, briquette mass and realistic sustained production.
Can long metal turnings go directly into a briquetting press?+
Long swarf should go directly into a press only when the exact inlet and feeding arrangement are approved for it. Tangled curls can create an inconsistent feed even when they can be pushed through an opening. Small Metal Turnings Shred-Briquetting Line illustrates a route with preparation; it should be compared with direct pressing using representative chip samples.
Send representative photos or samples of the actual swarf. The objective is a prepared chip form compatible with the inlet and feeding system, not the assumption that every press can accept an unrestricted machining-chip mixture.
How does variable-frequency screw feeding help a briquetting line?+
Variable-speed screw feeding helps coordinate delivery, but speed is not a direct mass-flow measurement. A change in chip density or screw fill can alter kilograms delivered at the same setting. Use an approved tuning method for the press; if the project needs accurate dosing, specify a suitable measuring and control arrangement separately.
- Confirm the screw's approved speed range.
- Check material movement at normal and low hopper levels.
- Observe whether the press is starved or over-supplied.
- Use only the approved coordination settings.
- Add a specified measuring arrangement if accurate mass dosing is required.
Screw speed alone does not establish precise mass flow. Bulk density, fill level and chip geometry influence delivery. A weighing or closed-loop metering requirement needs additional specified equipment rather than being assumed from speed control.
Why do briquette density and strength vary?+
Briquette density and handling strength are related but distinct results. A dense unit may still have unacceptable edges or break during transfer, while different alloys need separate assessment. Record both dimensions and mass at a defined stage and test the handling that matters; do not transfer a maximum density from another material.
Assess what the receiving process actually needs: manageable handling, density, dimensional stability or another property. Trials should measure the finished product under agreed conditions. Do not assume a catalogue density or an attractive sample proves the result for every production stream.
Related products
Hopper Type Shear Baler
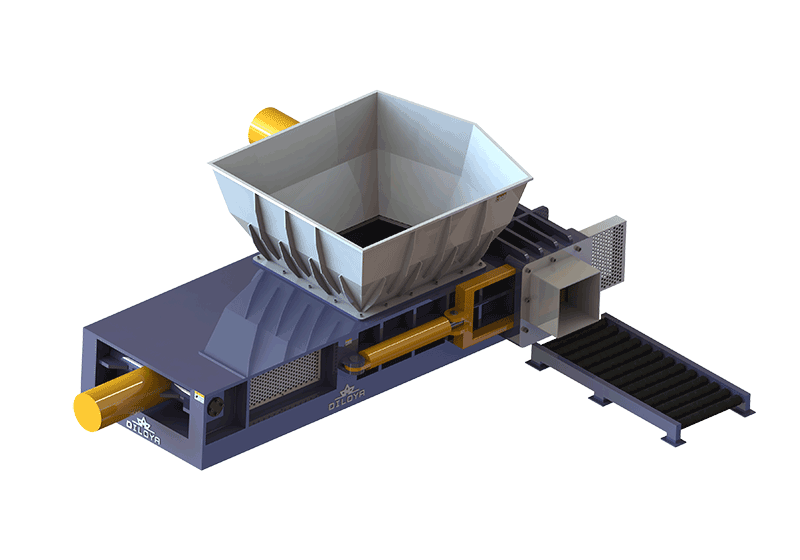
The Hopper Type Shear Baler is a heavy-duty hydraulic scrap processing machine designed for efficient shearing, compacting, and recycling of various metal scraps, aluminium tins cans, Scrap steel, light metal, sheet metal, profiles, pipes, and other bulky materials can be continuously loaded into the hopper and compressed before cutting.
View details +
Double Outlet Briquetting Press
The DILOYA Double Outlet Briquetting Press cold-compresses suitable metal chips into dense briquettes and uses two discharge outlets to support a planned collection flow. It is configured for recycling operations that need steady feeding and efficient removal of finished blocks.
View details +
Integrated Briquetting Press
The DILOYA Integrated Briquetting Press combines chip feeding, hydraulic compaction, briquette discharge and coordinated controls in one metal-chip recovery system. It turns sorted aluminium, copper, brass, cast-iron and other suitable machining chips into compact briquettes for easier handling and recycling.
View details +
Horizontal Briquetting Press
The DILOYA Horizontal Briquetting Press uses horizontal hydraulic compression to turn sorted machining chips and swarf into dense, manageable briquettes. It can be configured with controlled feeding, discharge and optional chip preparation for metalworking or recycling lines.
View details +
Vertical Briquetting Press
The DILOYA Vertical Briquetting Press uses a vertical hydraulic ram to cold-compress sorted aluminium, copper, brass, cast-iron and other suitable machining chips into dense briquettes. Its upright press layout supports organized chip recovery at workshops and recycling plants.
View details +Customer Cases
View all cases + Aluminium Chips Briquetting Machine
A Thai customer's 6061 aluminium chip briquetting project with reported output of 1,000–1,500 kg/hour, density above 2,000 kg/m³ and industrial oil cooling.
View case + Double Outlet Aluminium Chip Briquetting Press In Greece
A Greek customer requires 600–800 kg/hour aluminium chip processing. The recommended double-outlet press uses PLC automation, with a stated rate of 5–6 briquettes/minute.
View case + Aluminium Die Cast Chips Briquetting Line in Korea
An integrated briquetting line for a Korean customer's ADC12 aluminium die-cast chips, with a reported capacity of 200–300 kg/hour and a compact layout for limited production space.
View case +Leave A Message
Let's Figure Out The Best Solutions!
Tell us what you need.
Share your material, target hour capacity and other requirements. Our engineering team will reply with a suitable solutions.