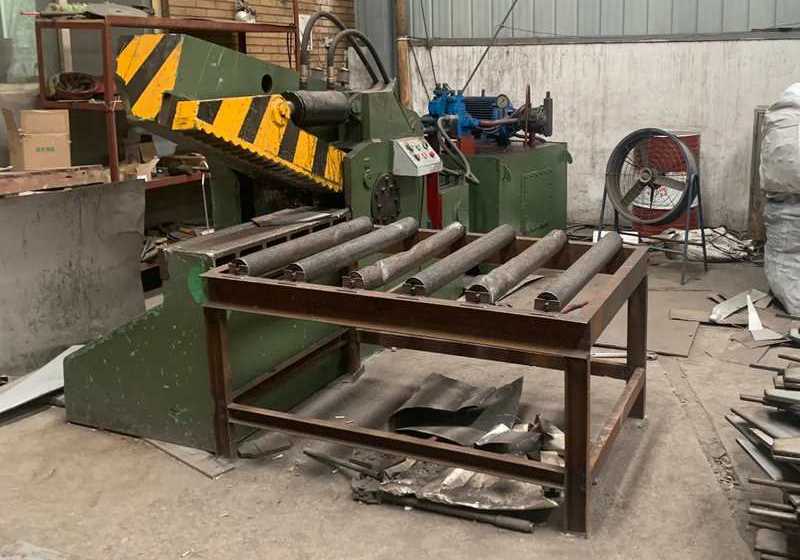
Alligator Shear
Traditional Heavy-Frame Hydraulic Alligator Shear
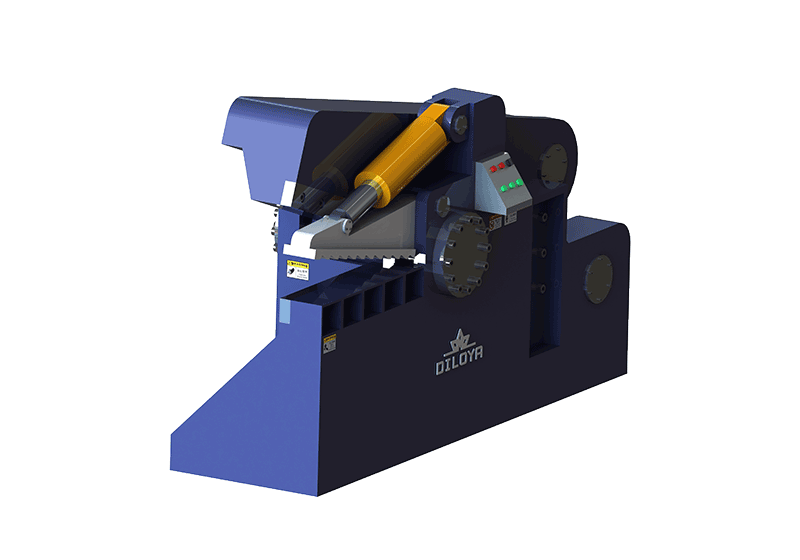
The DILOYA Alligator Shear is a conventional hydraulic pivot-jaw scrap cutter built for stable, repeatable cutting of suitable metal sections. Its robust frame and straightforward cutting arrangement serve scrap yards, fabrication shops and recycling operations preparing bars, pipes, profiles and offcuts for the next handling or processing stage.
- Model
- AS Series
- Output Capacity
- 300-5000kg/Hour
- Material
- Heavy Scrap Metal
- Control
- Button/Foot Control
- Power supply
- Customized
- Blade Materials
- H13, 9CrSi
Description
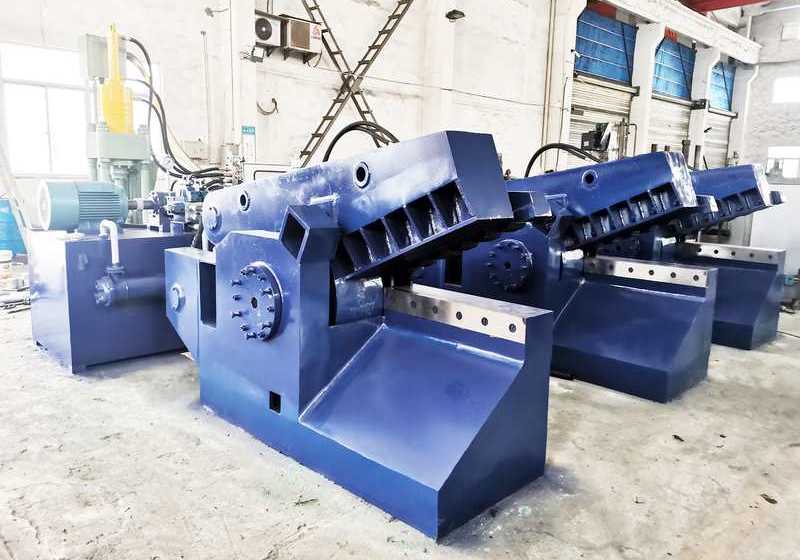
The DILOYA Alligator Shear follows the traditional pivoting-jaw design widely used to shorten metal scrap before sorting, loading, downstream shearing or remelting. A heavy frame supports the cutting bed and moving blade, while the hydraulic system supplies the force required for each stroke. Its straightforward mechanical layout is suited to operations that value a stable, durable cutting station.
1> How It Works
Operators position compatible scrap in the jaw and use the specified hold-down arrangement to control movement. The hydraulic cylinder closes the cutting arm, bringing the blade through the feed; the arm then opens for the next piece. Cutting bars, pipes, profiles or fabrication offcuts into shorter lengths can improve binning and subsequent handling. Feed must remain within the rated blade opening, section and material-strength limits.
2> Robustness and Service
The frame, pivot, cutting bed and blade arrangement are central to machine stability under repeated loads. Blade inspection, adjustment and replacement, lubrication, hydraulic-fluid care and checks of guards and controls remain essential. A strong frame is not a substitute for correct material selection or safe feeding practice.
3> Match the Machine to the Scrap
DILOYA can specify blade length, cutting force, mouth opening, motor power and controls around the site's typical and maximum piece sizes. Buyers should provide metal grade, cross-section, wall thickness, hourly volume and cut-length target so the chosen shear is not undersized or unnecessarily large.
Advantage
> Robust traditional structure: a heavy frame supports repeated hydraulic cutting loads.
> Stable cutting station: the pivoting jaw and defined cutting bed help control the workpiece.
> Established operating method: feed, clamp where specified, cut and reset in a clear sequence.
> Versatile metal preparation: suitable bars, pipes, profiles and offcuts can be cut to manageable lengths.
> Serviceable wear parts: blades and hydraulic components can be inspected and maintained as part of a planned schedule.
> Configurable duty: opening, blade length and force are selected for material section and required volume.
Parameter
Please find below specification of different models:
| Model | AS63 | AS100 | AS125 | AS160 | AS200 | AS250 | AS315 |
|---|---|---|---|---|---|---|---|
| Blade Length | 400mm | 600mm | 600mm | 700mm | 800mm | 1000mm | 1200mm |
| Max. Shear Froce | 630kn | 1000kn | 1250kn | 1600kn | 2000kn | 2500kn | 3150kn |
| Press Force | 120kn | 120kn | 200kn | 200kn | 250kn | 300kn | 500kn |
| Motor Power | 7.5kw | 11kw | 15kw | 18.5kw | 22kw | 30kw | 2x18.5kw |
| Cutting Frequency | 6-10times/Min | 6-10times/Min | 6-10times/Min | 6-10times/Min | 6-10times/Min | 6-10times/Min | 8-12times/Min |
| Table Height | 800mm | 800mm | 800mm | 800mm | 800mm | 800mm | 800mm |
| Control | Button Control | Button Control | Button Control | Button Control | Button Control | Button Control | Button Control |
| Cooling System | Fan Cooling | Fan Cooling | Fan Cooling | Fan Cooling | Fan Cooling | Fan Cooling | Fan Cooling |
We can customize the baler machine according to your special requirements.
Application
The DILOYA AS Seires alligator shear can cut below materials:
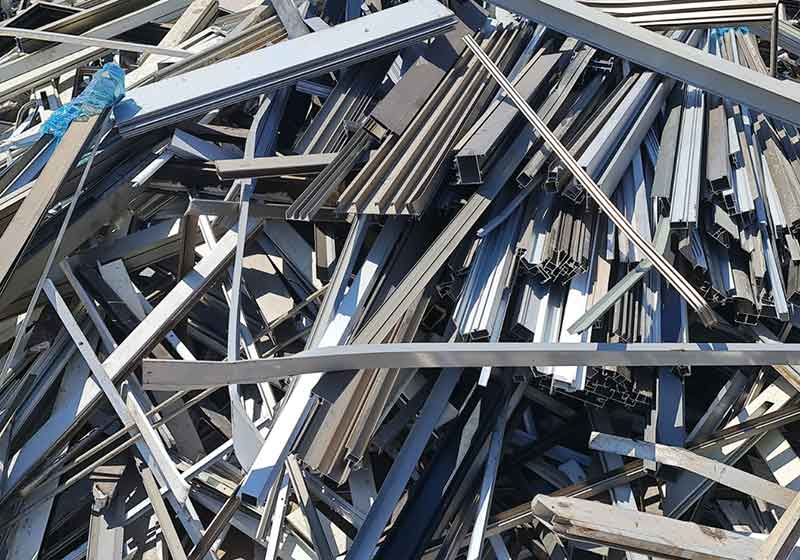
Aluminium Profiles
Aluminium profiles and extrusion offcuts are long, hollow and difficult to stack efficiently. DILOYA hydraulic metal balers compress window frames, structural sections and production offcuts into dense, stable bales for safer handling, lower storage and transport costs, and consistent delivery to aluminium recyclers and remelting plants.
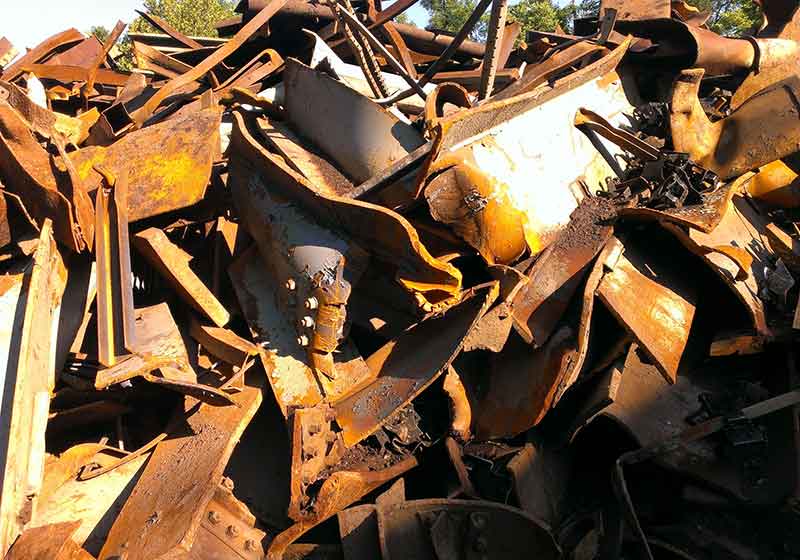
Heavy Scrap Metal
Heavy scrap metal includes thick steel plate, beams, channels, pipe, fabrication offcuts and dismantled machinery structures. DILOYA hydraulic scrap shears pre-compress and cut this oversized ferrous material into controlled furnace-ready lengths for safer stockpiling, efficient loading and reliable downstream melting. This application is intended for shearing only.
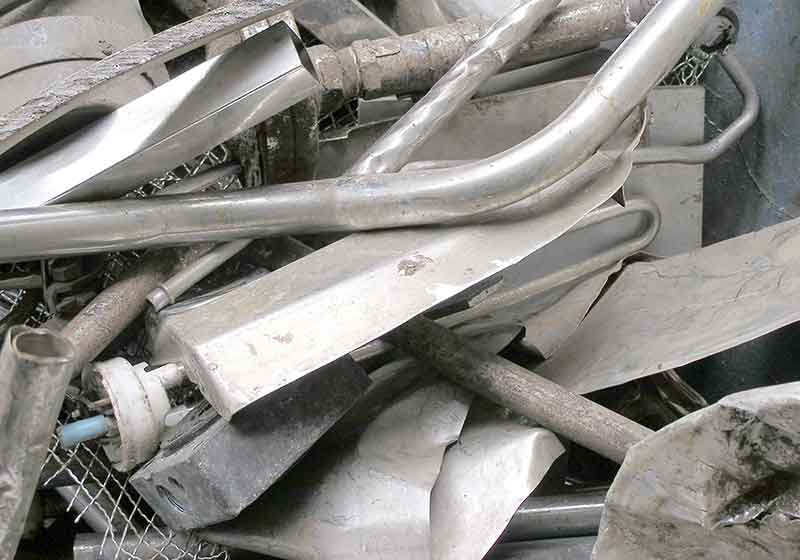
Stainless Steel Scrap
Stainless steel scrap includes sorted sheet offcuts, press skeletons, wire, mesh and light fabrication remnants. DILOYA hydraulic metal balers compress this valuable but bulky material into dense, stable bales while supporting grade separation, safer handling, compact storage and efficient shipment to stainless recyclers and melting plants. This application is intended for baling only.
Steel Bar
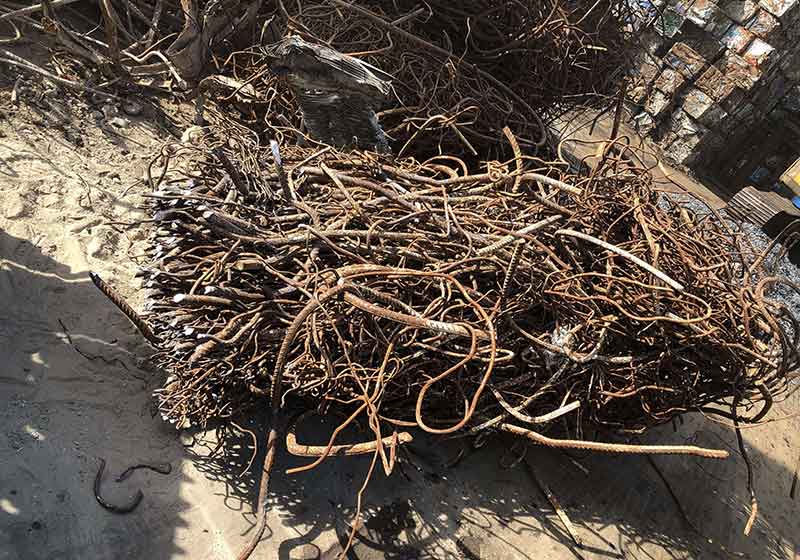
Steel bar scrap includes reinforcing bar, round bar, bent rod, short offcuts and tangled demolition rebar. DILOYA processes long or rigid bars with hydraulic scrap shears for controlled cut lengths, while shorter and bendable material can be compressed into dense transport bales with hydraulic metal balers. The correct route is selected from bar diameter, length, condition and downstream requirements.
FAQ
How should I compare alligator, gantry and other scrap-shear designs?+
Compare shear designs by their material-control and loading method before comparing force. Alligator Shear may address a different feed and handling duty from Vertical Gantry Shear. The right design is the one that accepts the approved sections consistently and delivers the required cut scrap without excessive repositioning or downstream waiting.
Compare each design against the same questions:
- What feed shape can it accept within its approved limits?
- How is material supported and controlled?
- How much repositioning is required?
- What finished size and sustained output are needed?
- How will cut scrap be removed?
Consider maximum section dimensions, material control during cutting, feeding effort, output size and the complete operating cycle. Submit representative scrap information so the proposed design can be assessed for the real workload and required protective arrangements.
How much cutting force does my material require?+
Cutting force must be assessed from the actual cross-section and material, not its outside dimensions alone. A hollow tube and a solid bar of the same diameter create different duties. Supply the difficult normal sections and known material properties so the proposed shear can be assessed as a complete blade, structure and hydraulic combination.
- Material grade or known strength.
- Solid, hollow or built-up cross-section.
- Maximum wall or plate thickness and width.
- How the piece is presented to the blades.
- Required cut length and sustained production.
Provide section drawings, thickness, alloy and maximum dimensions. The machine supplier should define approved material limits for the selected shear. Avoid treating a force number as permission to cut any object that fits.
Can one maximum-thickness figure describe every shear application?+
No single thickness figure covers every material and section. A plate rating without width or grade leaves out part of the cutting problem, just as tube diameter leaves out wall thickness. Ask for the reference section behind the rating and the approved limits for your scrap before assuming equivalent capability.
Why geometry matters: a tube's outside diameter does not describe its wall thickness, and a plate's thickness does not describe its width. A rating based on one reference section cannot be transferred directly to a different shape.
Submit the largest and most demanding normal sections, including drawings where available, for an application-specific assessment.
Ask what reference material and geometry support the rating. For mixed scrap, identify the difficult sections and assess them explicitly. The approved operating envelope is more useful than a single headline maximum.
How does blade condition influence cutting performance?+
Blade condition affects the way load is transferred into the material. A deteriorating cut can therefore be a maintenance warning rather than a sign that greater pressure is needed. Record the material and symptoms, then have qualified personnel assess the approved blade and setup limits. A fixed lifetime cannot be inferred without the actual duty.
Do not use increased hydraulic pressure to compensate for an unexplained decline in cutting performance. Qualified personnel should assess blade condition and the machine setup. Wear life depends on scrap quality, duty and contamination rather than a universal operating-hour figure.
Which objects need exclusion or special assessment before shearing?+
Hazardous or unidentified objects must be segregated before the cutting stage. A metal exterior does not establish that a container is empty, depressurised or free of reactive contents. The approved scrap specification and site acceptance procedure should also exclude sections outside the machine's strength and dimensional limits.
Also identify objects outside the approved strength or dimensional limits. Material inspection and the site's acceptance procedure are part of safe scrap preparation. Never use the shear to discover what an unidentified object contains.
Related products
Horizontal Container Shear
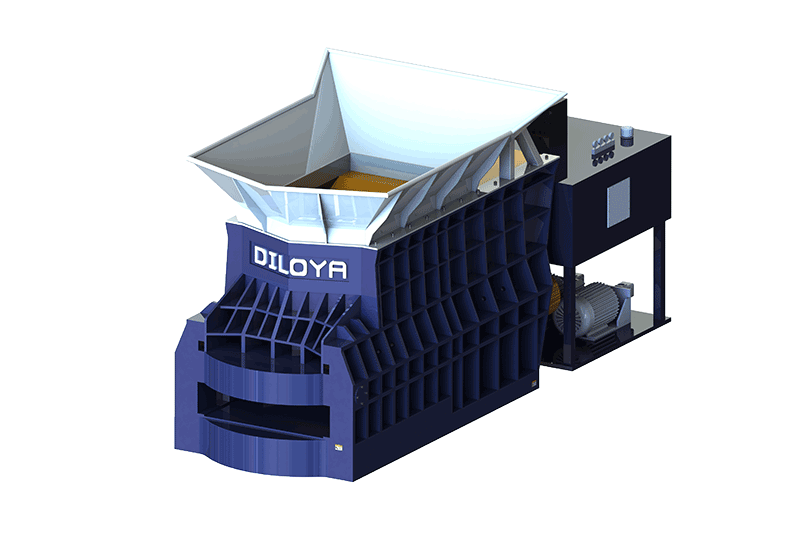
The DILOYA Horizontal Container Shear uses a box-style receiving chamber to contain, compress and shear bulky steel scrap in a planned production sequence. Its horizontal layout is intended for high-volume scrap yards that need strong cutting performance while using the available site area efficiently. Heavy plate, structural sections and other compatible ferrous scrap are assessed against chamber dimensions and cutting force.
View details +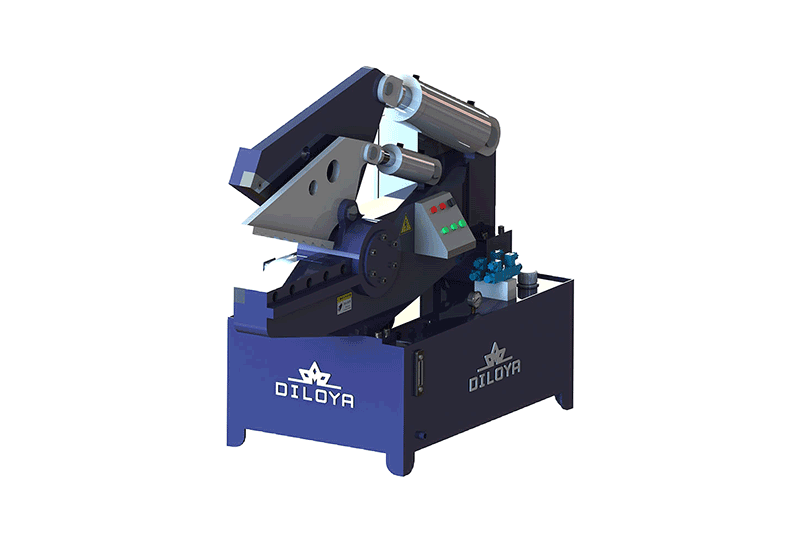
Integrated Alligator Shear
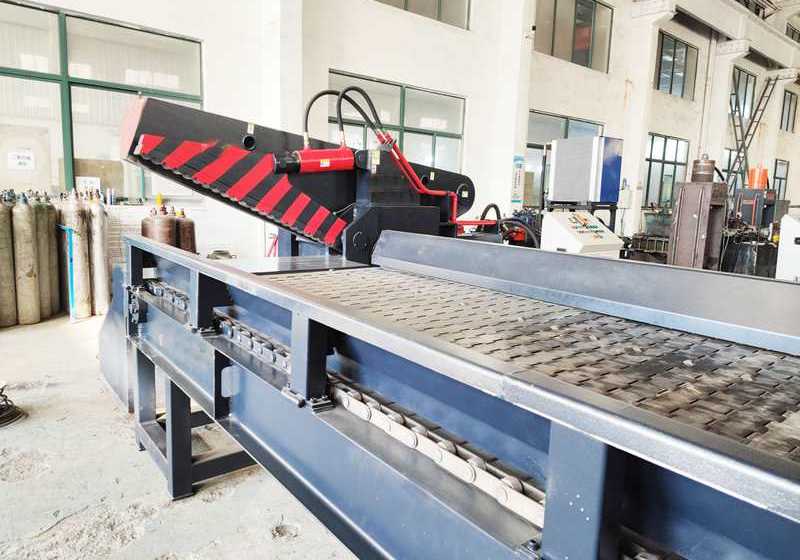
The DILOYA Integrated Alligator Shear refines the conventional alligator-shear arrangement into a more compact, coordinated machine package. It cuts suitable scrap bars, profiles, tubes and production offcuts while reducing the installation space and external component layout required by a traditional setup. The exact integrated functions and cutting range depend on the selected model.
View details +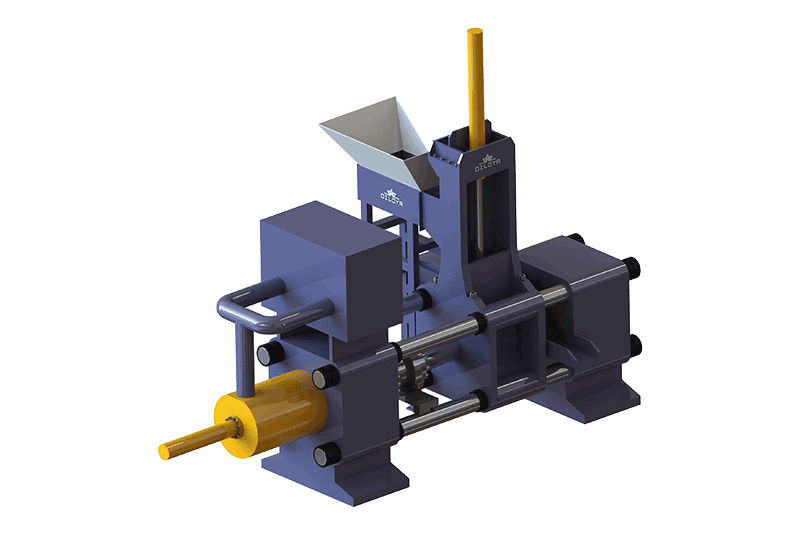
Horizontal Briquetting Press
The DILOYA Horizontal Briquetting Press uses horizontal hydraulic compression to turn sorted machining chips and swarf into dense, manageable briquettes. It can be configured with controlled feeding, discharge and optional chip preparation for metalworking or recycling lines.
View details +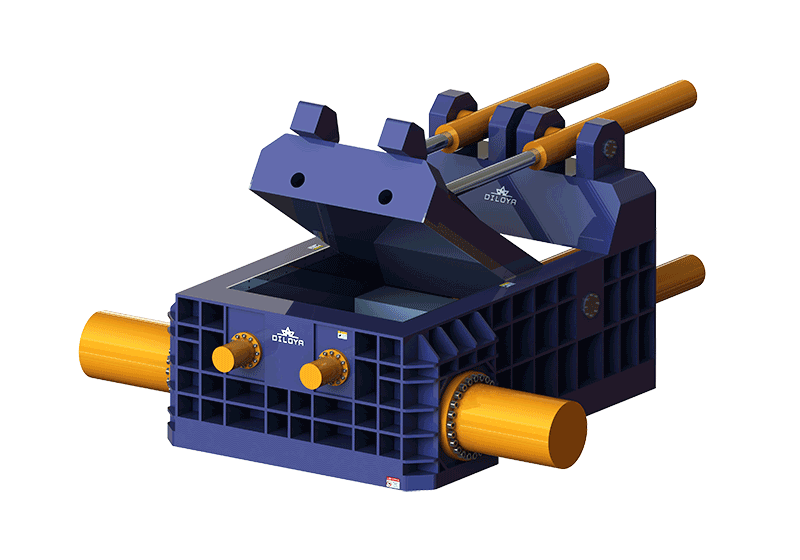
Heavy Duty Metal Baler
The DILOYA Heavy Duty Metal Baler uses two main hydraulic cylinders to compact bulky scrap metal into dense, rectangular bales. Finished bales are removed by grab for storage, loading and downstream recycling.
View details +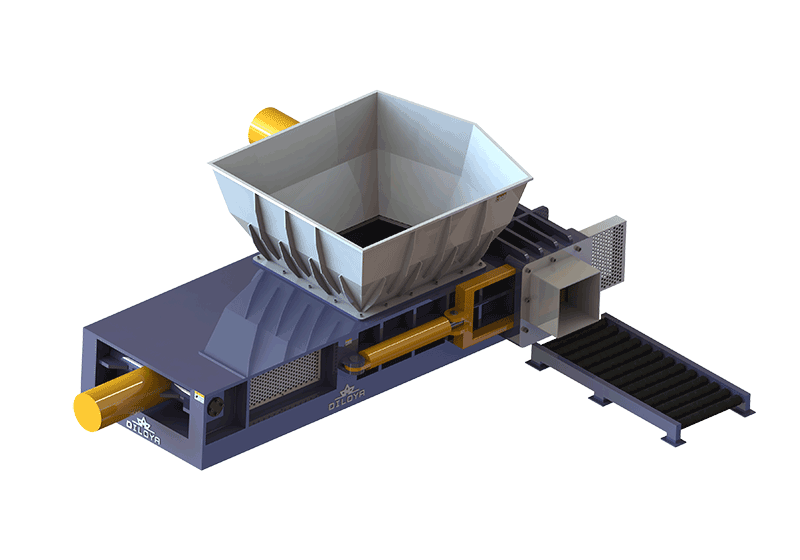
Hopper Type Shear Baler
The Hopper Type Shear Baler is a heavy-duty hydraulic scrap processing machine designed for efficient shearing, compacting, and recycling of various metal scraps, aluminium tins cans, Scrap steel, light metal, sheet metal, profiles, pipes, and other bulky materials can be continuously loaded into the hopper and compressed before cutting.
View details +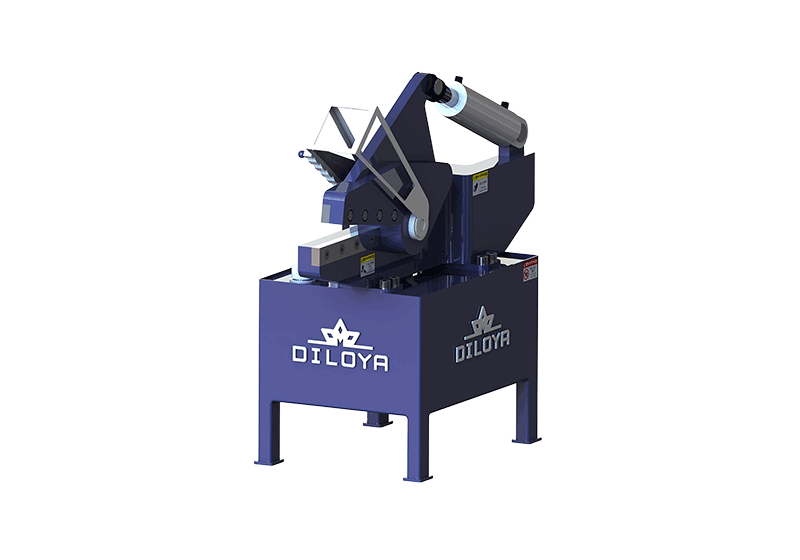
Mini Alligator Shear
The DILOYA Mini Alligator Shear is a compact, movable hydraulic cutting machine for light and relatively thin scrap. It helps workshops and collection points cut small-diameter cable and wire, aluminium profiles, copper tube and other suitable non-ferrous offcuts into manageable lengths. The machine is selected according to material cross-section, wall thickness and cutting-force requirements.
View details +Customer Cases
View all cases + Alligator Shear For Aluminium Ingot Cutting In South Africa
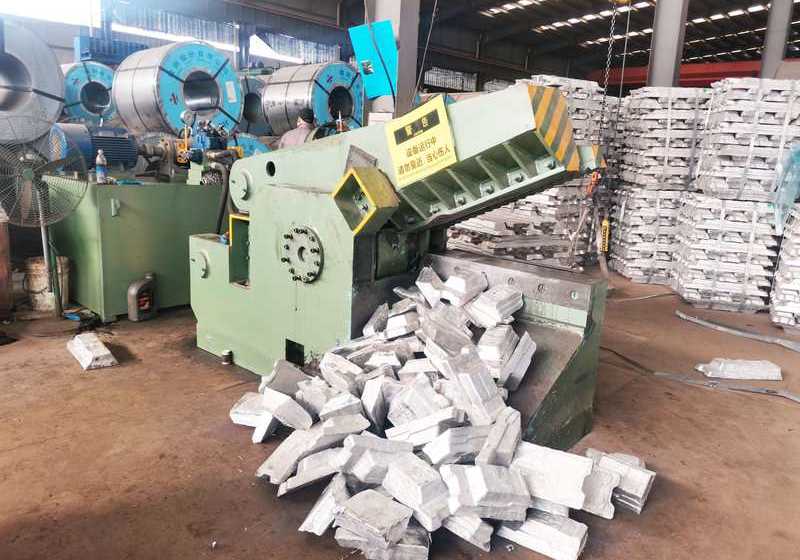
A South African customer uses a conventional Alligator Shear for aluminium ingots, with reported output of 800–1,000 kg/hour and 8–12 cutting strokes/minute.
View case + Horizontal Steel Bar Container Shear For Heavy Scrap In Singapore
Singapore customer case: a horizontal box shear for waste rebar and heavy structural steel, with reported output of 10–15 t/hour, PLC automation and remote control.
View case + Automatic Side Turn-Out Metal Baler For Aluminium Profiles In The UAE
A UAE customer reports 2,000–2,500 kg/hour aluminium-profile baling and density up to 1,000 kg/m³, then orders two more identical balers after two months.
View case + Big Output Horizontal Briquetting Line
A Russian iron chip briquetting project with a reported output of 4,000–6,000 kg/hour and briquette density of 5,000 kg/m³, supporting organised handling, storage and recycling.
View case + Double Outlet Aluminium Chip Briquetting Press In Greece
A Greek customer requires 600–800 kg/hour aluminium chip processing. The recommended double-outlet press uses PLC automation, with a stated rate of 5–6 briquettes/minute.
View case +Leave A Message
Let's Figure Out The Best Solutions!
Tell us what you need.
Share your material, target hour capacity and other requirements. Our engineering team will reply with a suitable solutions.