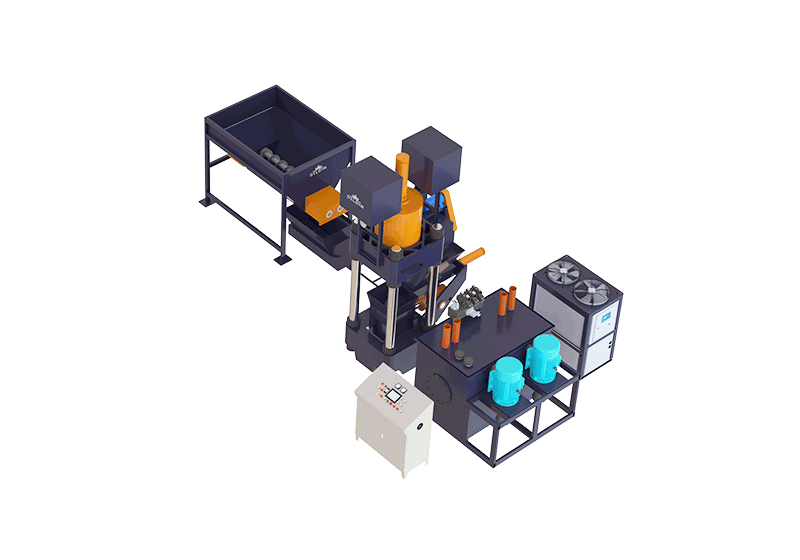
High-output briquetting for free-flowing metal granules and short chips
The DILOYA Short Metal Chips Briquetting Solution is designed for metal feedstocks with good flowability, including copper granules, copper rice, aluminum granules and suitable cast iron chips. The line combines a large screw-equipped buffer hopper, controlled screw feeding and hydraulic briquetting to process prepared material through an automated production sequence.
Rather than adding small quantities directly to the press at frequent intervals, the operator loads material into the large buffer hopper. The hopper stores a working reserve, and the screw feeding system transfers it to the briquetting machine as required. This arrangement reduces loading frequency and supports high-output operation with less repeated manual feeding.
Suitable materials and feed characteristics
This solution is intended primarily for short, granular or otherwise free-flowing metal material. The important consideration is not only the metal grade, but whether the material can move through the hopper and screw system consistently.
> Copper rice and copper granules: prepared granular copper feed, assessed for particle size, cleanliness, bulk density and remaining non-metallic contamination.
> luminum granules: suitable free-flowing aluminum or aluminium particles, with the press and feed arrangement selected for the actual alloy and material condition.
> Cast iron chips: short cast iron machining chips suitable for screw feeding and compression, assessed for particle distribution, coolant content and contaminants.
> Other short metal chips: additional materials can be evaluated using representative samples before the line configuration is confirmed.
Different metals and alloy grades should be processed separately according to the customer's recycling requirements. Long, curled and tangled turnings are not equivalent to free-flowing granules: they may need shredding or other preparation before they can be handled reliably by this type of line. A shredder is not a standard process stage for material that is already suitably sized and free-flowing.
Process flow: bulk loading, buffering, screw feeding and briquetting
1> Prepare and load the feedstock. Suitable material is added to the large buffer hopper using the customer's agreed loading method. Oversized pieces and foreign objects should be removed before feeding.
2> Build a working material reserve. The hopper temporarily stores the feedstock between loading events. Its working volume is matched to the material's loose bulk density, the required output and the desired time between refills.
3> Meter material through the screw system. The hopper screw and conveying arrangement deliver material toward the press. The feeding sequence is coordinated with the briquetting machine's demand rather than relying on repeated manual loading of each pressing cycle.
4> Hydraulically compress the material. The press receives a controlled charge and forms it into a compact briquette. Press configuration and operating settings are selected for the material and required production rate.
5> Discharge and collect the briquettes. Finished briquettes leave the press for collection or onward handling. The discharge arrangement and collection capacity should be matched to sustained production.
A large screw hopper reduces loading frequency
The buffer hopper allows material to be loaded in larger batches while the press consumes it progressively. This helps separate the operator's loading schedule from the repeated feed-and-press cycles of the briquetting machine. Staff can replenish the hopper when required rather than remain beside the feed opening throughout the production run.
The actual refill interval depends on usable hopper volume, material bulk density and the line's consumption rate. A hopper filled with light aluminum particles will not contain the same mass as one filled to the same volume with denser copper material. For this reason, hopper sizing must be based on the actual feedstock and target operating pattern, not a single nominal volume alone.
Good flowability is central to this arrangement. Hopper geometry, screw dimensions, drive selection and discharge design must work together for the supplied material. Representative material trials help identify whether additional preparation or a different feeding arrangement is required.
High automation and coordinated production
The line integrates material buffering, screw feeding and hydraulic compression into a coordinated process. The control specification can link feeding demand, material availability and the press cycle so that material moves through the system in the intended sequence. Level monitoring and relevant interlocks can be specified as part of the final configuration.
This reduces repetitive handling between separate equipment stages and supports more consistent operation. Operators still manage material supply, monitor the line, remove collected briquettes and perform inspection, cleaning and maintenance. High automation should be understood as reducing repeated manual feeding, not eliminating the need for trained personnel.
Production capacity up to 2–3 tonnes per hour
With a suitable material and matched equipment configuration, line capacity can reach 2–3 tonnes per hour (2,000–3,000 kg/h). This high-output arrangement is intended for customers with a substantial supply of suitable short chips or granular metal material and a need for automated feeding and briquetting.
The stated range is a configuration-dependent capacity, not a guaranteed output for every material. Actual throughput depends on metal type, bulk density, particle size and distribution, moisture or coolant content, feeding behavior, briquette requirements and the selected press. DILOYA should confirm the achievable production rate for the customer's representative material and operating conditions.
To sustain the target output, the entire handling chain must be considered. Loading capability, hopper replenishment, screw delivery and briquette collection must all support the required mass flow. A high-capacity press alone cannot maintain production if material supply or finished-briquette removal becomes the limiting stage.
Practical benefits for the workshop
> Fewer loading events: the large hopper holds a working reserve and reduces the need to add small batches repeatedly.
> Less repetitive manual feeding: screw handling moves suitable material from storage to the press.
> High-output configuration: the feeding system and briquetting machine can be selected together for the required production target.
> Integrated operation: buffering, conveying and compression are arranged as one coordinated line.
> Organized downstream handling: briquette discharge and collection can be planned around the workshop's recycling workflow.
Configure the line for your material and output target
Provide the metal and alloy, particle photos or samples, approximate bulk density, moisture or coolant condition, available feed quantity per shift, target hourly output and preferred briquette size. The proposal should also consider the loading method, refill interval, available floor area and clear height, electrical supply, maintenance access and finished-briquette collection.
DILOYA can then match the buffer hopper, screw feeding arrangement and briquetting press to the actual application. Hopper capacity, line dimensions, installed power and confirmed throughput should be stated in the project-specific quotation, with any optional preparation, fluid collection or discharge equipment identified separately.