Cast Iron Chips

Cast iron chips are fine, brittle machining residues that are abrasive, dusty and difficult to store or charge in loose form. DILOYA hydraulic briquetting presses compress grey-iron and ductile-iron swarf into dense cylindrical briquettes while recovering part of the retained cutting fluid for cleaner handling, efficient transport and controlled foundry feeding. This application is intended for briquetting only.

What our engineers evaluate

Our engineers evaluate cast iron grade, particle-size distribution, fines percentage, loose bulk density, moisture and oil content, abrasiveness, contamination, required throughput, briquette diameter and density, feeding continuity, fluid recovery requirements, installation space and local voltage.

Discuss your application +
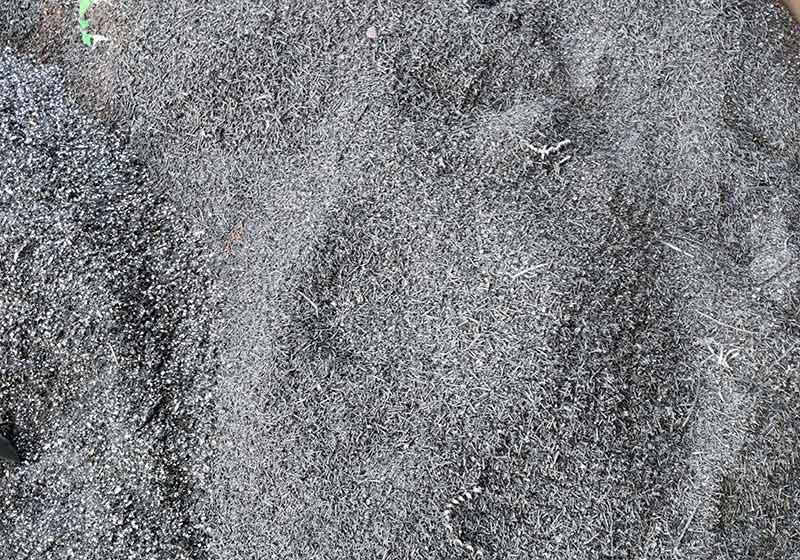
Loose fine cast iron machining chips

Cast iron chips are fine, brittle machining residues generated when turning, milling, boring or drilling cast components such as engine blocks, brake parts, pump housings and machine beds. The material often contains short needle-like fragments, powdery fines and retained cutting fluid. In loose form it occupies excessive space, leaks through containers and is difficult to charge into a furnace efficiently.

DILOYA hydraulic briquetting presses compact cast iron chips into dense cylindrical briquettes. The pressure creates stable units for cleaner storage and transport while expressing part of the oil or coolant for recovery. This application is intended for briquetting only and is engineered separately from baling sheet scrap or shearing structural steel.

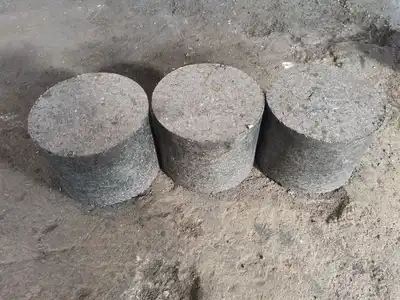
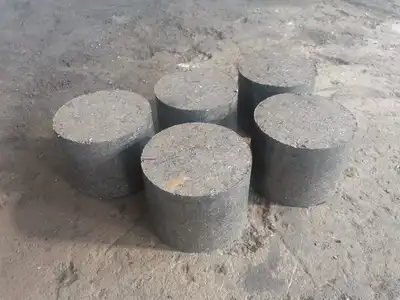
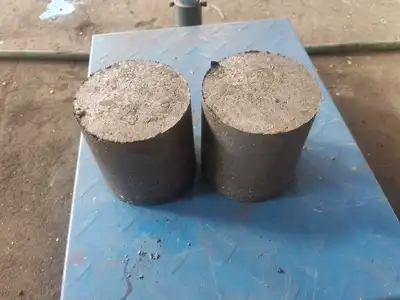
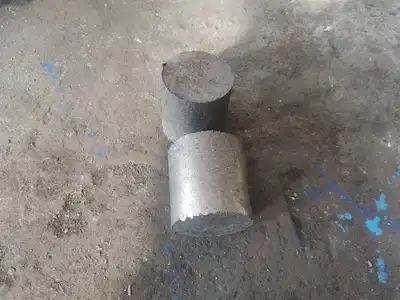
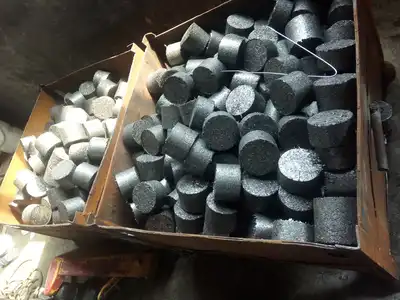
Effect After Cast Iron Chip Briquetting

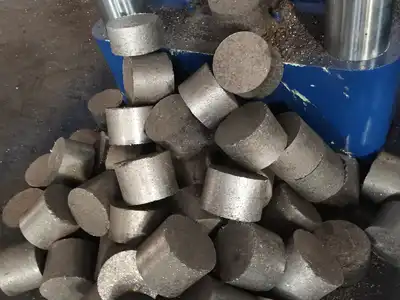
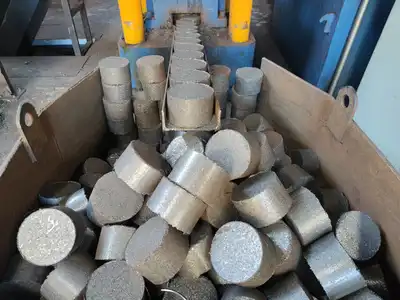
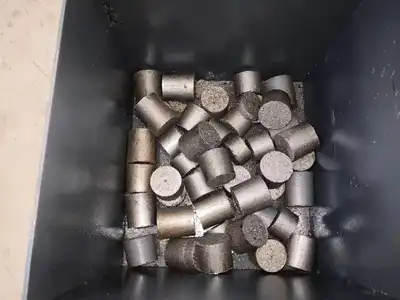
Cast iron chip briquettes collected in a steel bin Three dense cast iron swarf briquettes Four cylindrical cast iron chip briquettes Paired cast iron briquettes after hydraulic pressing
Cast iron briquette samples showing stable compact form Cast iron briquettes discharged beside the briquetting press Continuous cast iron briquette output collection Finished cast iron chip briquettes in a collection box

Suitable Cast Iron Chip Feed

Typical feed includes grey-iron turnings, ductile-iron chips, short brittle swarf and screened cast-iron fines from machining operations. The best results come from a consistent grade with controlled particle size and moisture. Oversized tramp metal, grinding media, rags, sand cores and non-ferrous contamination should be removed before the material reaches the press.

Cast iron chips are generally shorter and less springy than long steel turnings, but they can contain a high proportion of abrasive fines. The hopper, screw feeder, chamber liners and seals must therefore be selected for reliable flow and wear resistance.

Benefits of Briquetting Cast Iron Chips

  • Dense compact output: reduces storage footprint and increases truck or container payload.
  • Cleaner work areas: controls dusty fines and prevents small chips from escaping open bins.
  • Recoverable fluids: separates part of the retained oil or coolant for collection, treatment or reuse.
  • More consistent furnace charging: briquettes are easier to meter and less likely to scatter than loose chips.
  • Lower oxidation loss: compact material has less exposed surface area than loose fine swarf during handling and melting.

Typical Briquetting Process

  1. Collect cast iron chips separately and remove incompatible grades and foreign objects.
  2. Screen or condition the feed when excessive fines, large fragments or free liquid are present.
  3. Meter chips from the storage hopper into the hydraulic compression chamber.
  4. Compress the material at controlled pressure and dwell time to form a stable briquette.
  5. Collect expressed fluid and discharge finished briquettes for cooling, storage or direct shipment.

Wear, Feeding and Fluid Control

Fine cast iron is abrasive, so replaceable liners, hardened wear components, effective hydraulic filtration and accessible cleaning points are important. A stable metering system prevents underfilled or overfilled cycles, while dust containment and housekeeping reduce accumulation around the hopper and press.

Free oil or coolant should be measured rather than estimated. The receiving tank, filtration and drainage arrangement must match the liquid volume, and recovered fluid should be handled according to the plant's environmental and safety procedures.

What DILOYA Engineers Evaluate

DILOYA evaluates cast iron grade, chip particle-size distribution, fines percentage, loose bulk density, moisture and oil content, abrasiveness, contamination, hourly throughput, target briquette diameter and density, feeding continuity, fluid recovery, installation space and local electrical supply.

Send representative chip photos or samples, daily volume, coolant information and downstream foundry requirements. Our engineers will match press force, chamber diameter, hopper, feeder, wear protection, hydraulic power, cooling and fluid collection to the actual cast-iron chip stream.
FAQ

How do I choose the right recycling process for my material?+

The right process is the one that produces a material your next customer or production stage can use. Bulky offcuts intended for transport need a different route from oily machining chips intended for remelting. Define that destination first, then work backwards through sorting, size reduction and compaction. How to Choose a Metal Chip Briquetting Line for a Small CNC Machine Shop illustrates why the upstream chip condition matters as much as the final press.

Baling, shearing, shredding and briquetting solve different handling problems. Send representative photos or samples and the buyer's acceptance requirements so the proposed process can be matched to both the incoming waste and its next use.

What information should I send for an accurate quotation?+

An accurate quotation needs an operating brief, not just a requested tonnage. Show the supplier the most difficult normal feed, describe the accepted finished product and identify the equipment already available at the site. Two quotations labelled “one tonne per hour” can cover very different processing stages; the information below helps make their scope comparable.

Useful information to include

  • Feed: material, size, contamination and sample photos.
  • Workload: daily mass, peak accumulation and available production hours.
  • Result: required package or cut size and the receiver's acceptance criteria.
  • Interfaces: loading method, collection equipment and any existing machines.
  • Site: layout, supply voltage, ambient conditions and destination.

Explain how material will arrive and how finished products will be removed. A floor plan, loading height and downstream equipment details help define the scope. The quotation should clearly distinguish the main machine, options, installation requirements and services.

How should I calculate the capacity my operation needs?+

Calculate demand from accepted processed mass divided by genuinely available production time. Then check peak accumulation separately: a line may meet the daily average yet fall behind during the busiest shift. Do not add an arbitrary safety margin before finding whether feeding, preparation or discharge is the real constraint. For chip-processing projects, How to Choose a Metal Chip Briquetting Line for a Small CNC Machine Shop explains the whole-line approach.

Example: processing 8 tonnes in 8 genuinely available production hours requires an average of 1 tonne/hour. If only 6 hours remain after the necessary tasks and interruptions, the required average during those hours is higher. These values illustrate planning, not a machine rating.

Use realistic measured availability and identify whether the proposed capacity includes all required handling stages.

Also consider the complete line. A fast press cannot compensate for an undersized shredder, slow bag placement or restricted discharge. State both average demand and peak accumulation so working buffers and sustained capacity can be selected sensibly.

Leave A Message

Let's Figure Out The Best Solutions!

Tell us what you need.

Share your material, target hour capacity and other requirements. Our engineering team will reply with a suitable solutions.

01Call DILOYA+86 152 2134 765002Email our teaminfo@diloya.com
We use your details to respond to this enquiry. Read our Privacy Policy.