A screw buffer is valuable when it creates a usable working reserve between intermittent replenishment and press consumption. Its geometric volume is not its useful stored mass, especially with fluffy chips. Storage Screw Hopper should be sized around material flow and a realistic refill interval, not used to conceal a permanent shortage of upstream capacity.
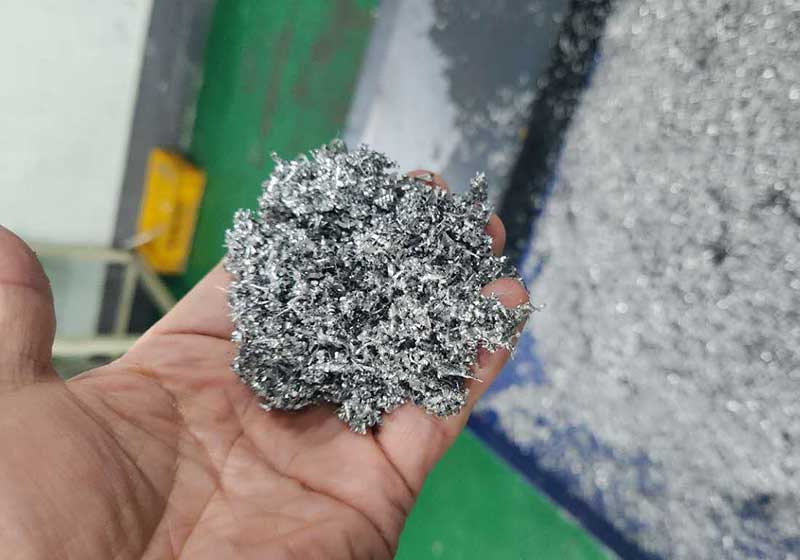
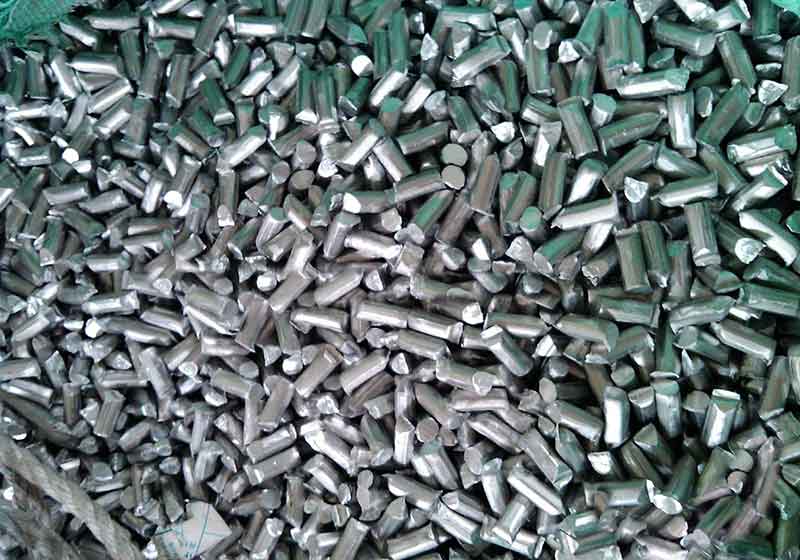
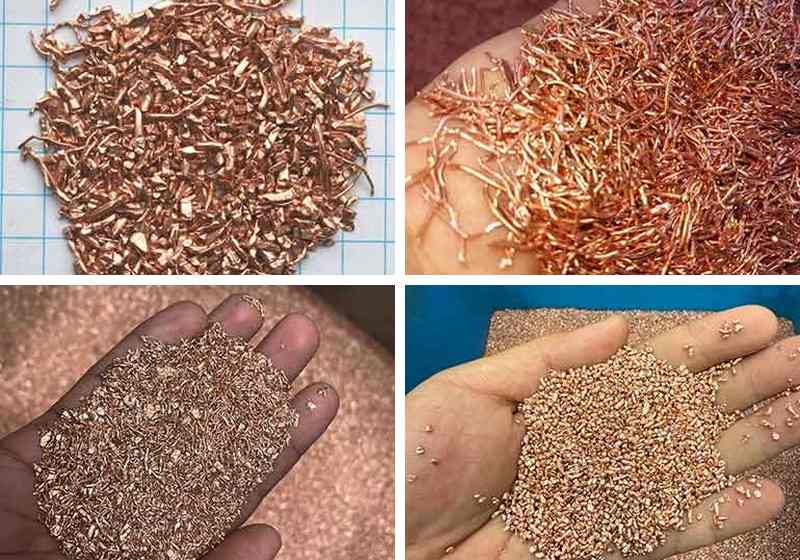
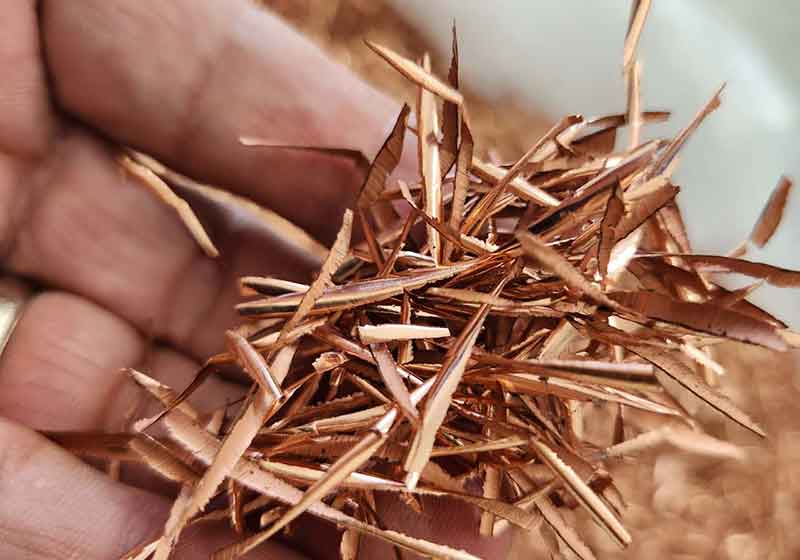
Planning relationship: usable buffer mass depends on usable hopper volume and the actual loose bulk density. The same hopper therefore stores different masses of fluffy aluminium swarf and denser short chips.
Estimate the replenishment interval from that working reserve and the press's measured consumption. Leave the operating allowance specified for material flow and control rather than treating the geometric hopper volume as fully usable storage.
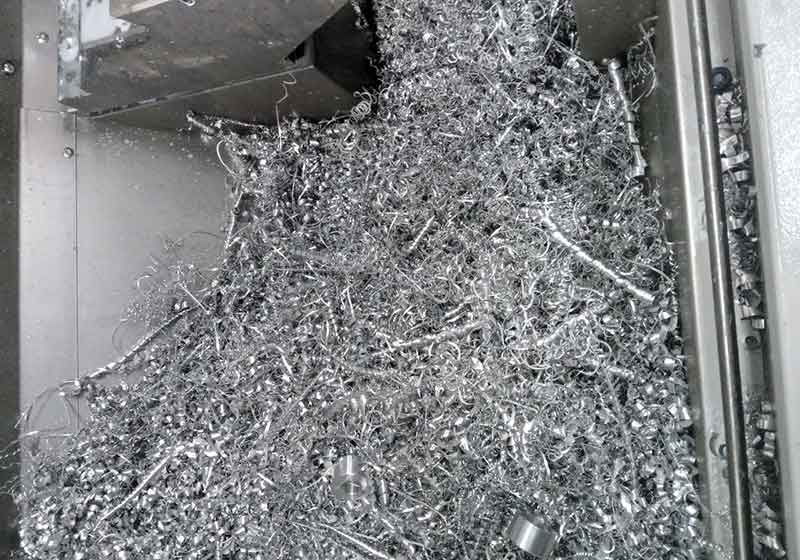
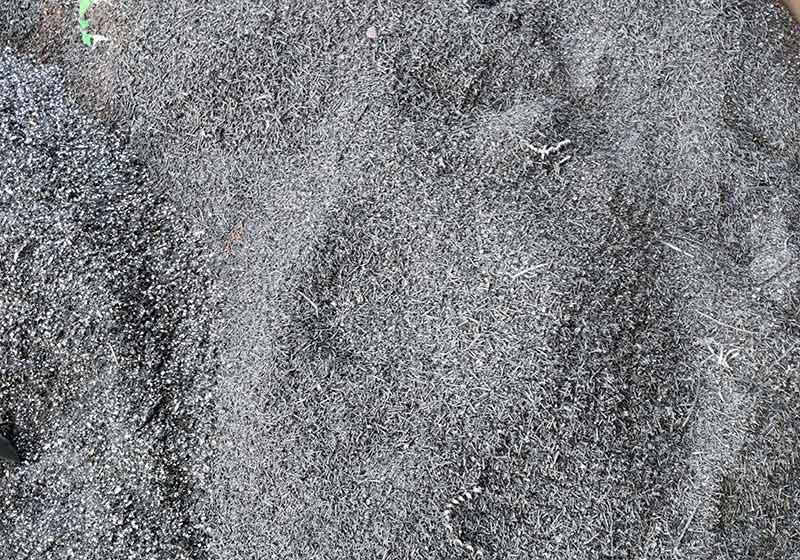
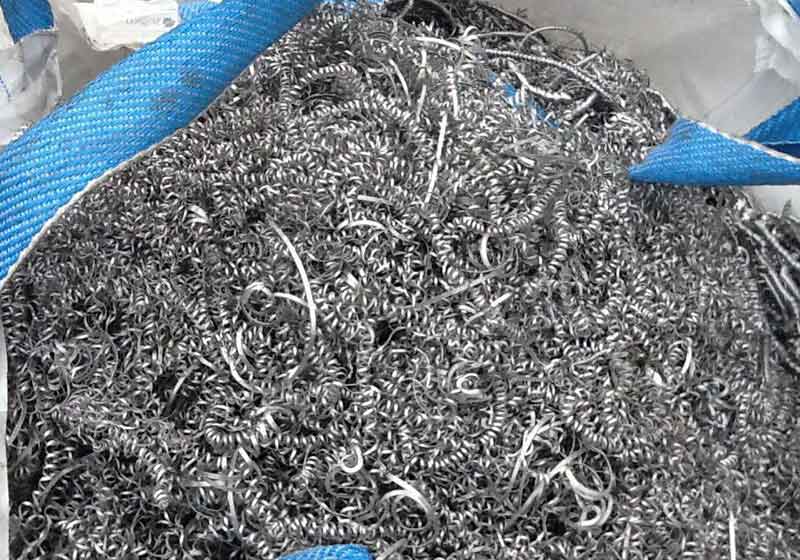
The usable volume, material flow and feed rate must match the actual chips. A buffer cannot compensate indefinitely if average upstream output is below press demand. Long tangled material may require preparation before entering the screw hopper.


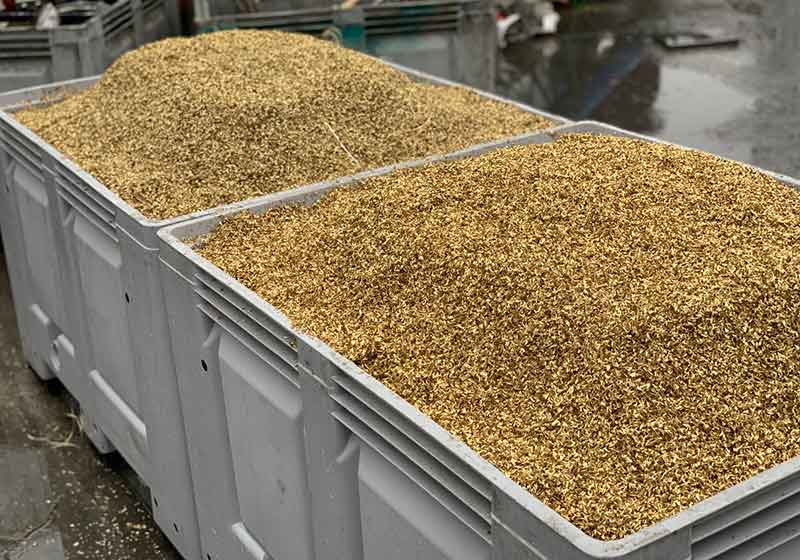
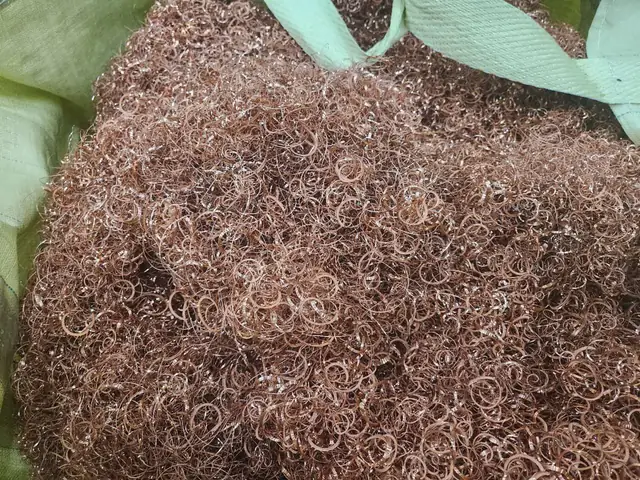
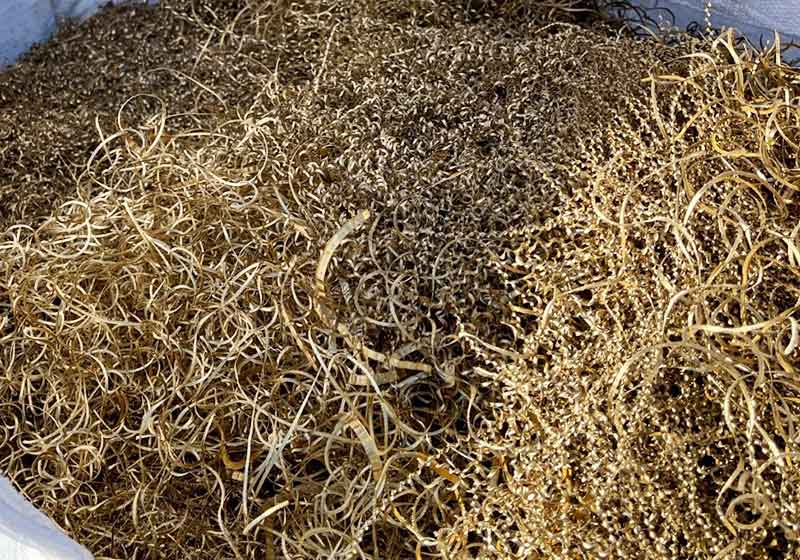


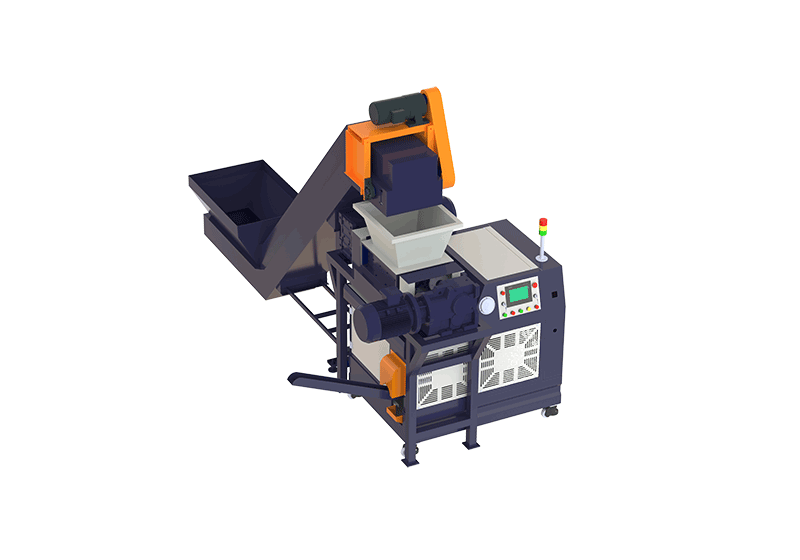 Small Metal Turnings Shred-Briquetting Line
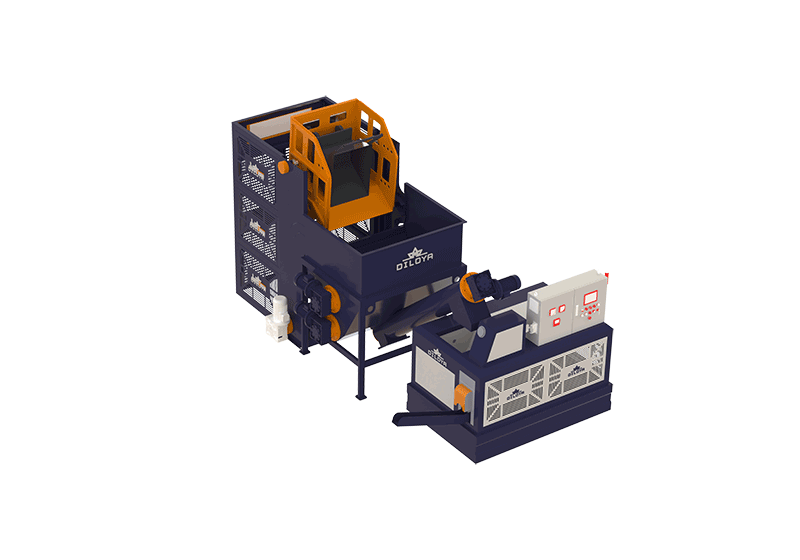 Integrated Auto Metal Chips Briquetting Line
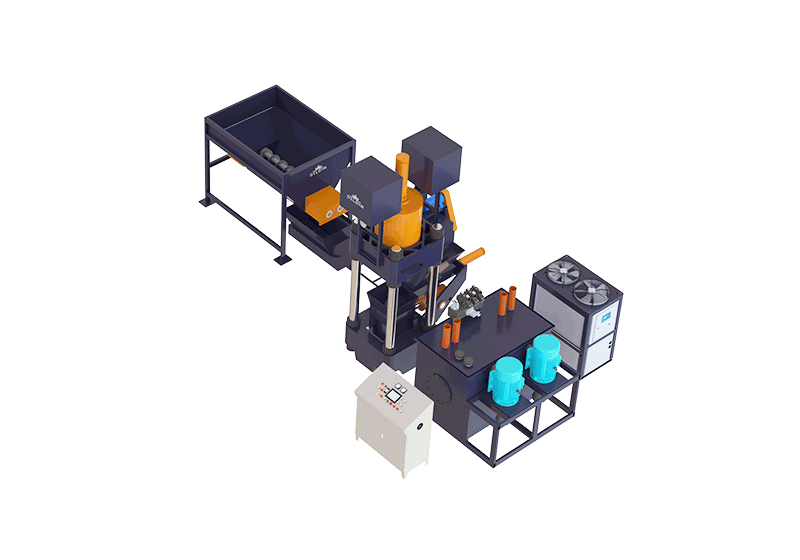 Short Metal Chips Briquetting Solution
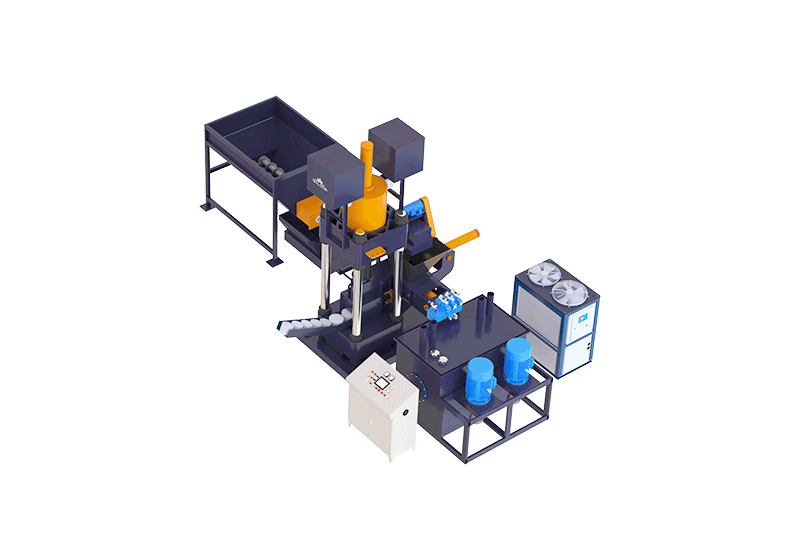 Aluminium Chips Briquetting Line